
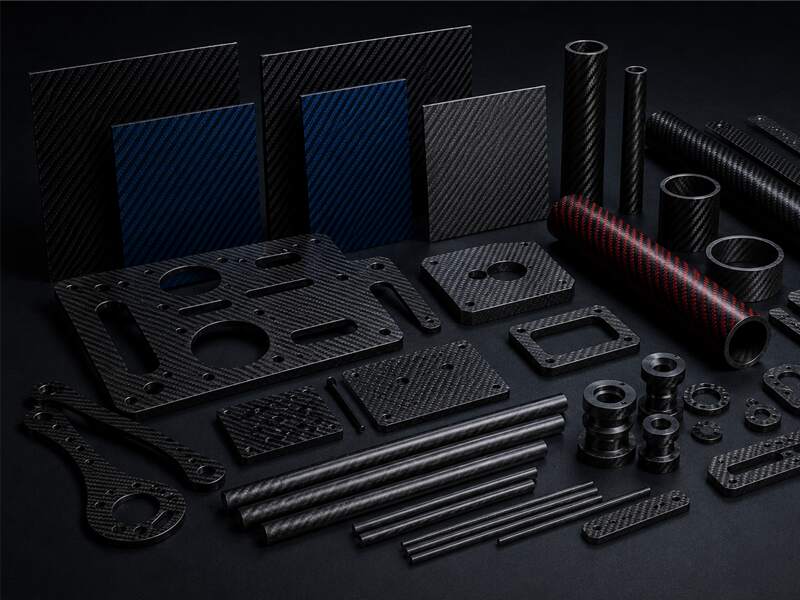
Carbon fiber can reduce environmental impact in some uses, but its production and end-of-life routes matter.
Carbon fiber is not automatically environmentally friendly. Its impact depends on several factors:
- Precursor chemistry
- Furnace energy and electricity mix
- Resin system and curing method
- Scrap control during cutting and molding
- Repair, recycling, or disposal route
A lightweight CFRP component can offset production emissions when it reduces fuel or energy use during service. Poorly designed laminates, rejected parts, and landfill disposal can remove that benefit.
Carbon fiber can be greener when high stiffness allows a lighter structure with long service life. This is most relevant in aircraft, wind blades, and moving vehicle parts.
Carbon Fiber Life Cycle
A life cycle view separates production impact from use-phase savings and end-of-life treatment.
Cradle to Gate and Cradle to Grave
Cradle to gate covers precursor production, fiber conversion, fabric formation, resin handling, and part molding. It helps compare material manufacturing before the product enters service.
Cradle to grave also includes use, repair, recycling, energy recovery, or landfill. This wider boundary is essential for carbon fiber because lightweighting benefits occur during service.
| Boundary | What It Includes | Why It Matters |
|---|---|---|
| Cradle to gate | Precursor, fiber, fabric, resin, and molding | Compares production impact |
| Cradle to grave | Production, use, repair, recycling, and disposal | Captures use-phase savings |
| Use phase | Fuel, electricity, fatigue life, and service duration | Shows lightweighting payback |
Carbon Footprint, Energy Use, and Landfill Risk
The carbon footprint of CFRP is driven by precursor energy, carbonization energy, resin chemistry, and process yield. Scrap from trimming, expired prepreg, and rejected laminates increases impact quickly.
Main impact drivers include:
- High energy demand during precursor conversion and carbonization
- Resin chemistry and cure temperature
- Expired prepreg, trimming scrap, and rejected parts
- Low process yield and poor furnace utilization
- Landfill risk for thermoset CFRP
Landfill risk is higher for thermoset CFRP because the crosslinked matrix does not remelt. End-of-life planning should be specified during material selection, not after production.
Carbon Fiber Manufacturing Impact
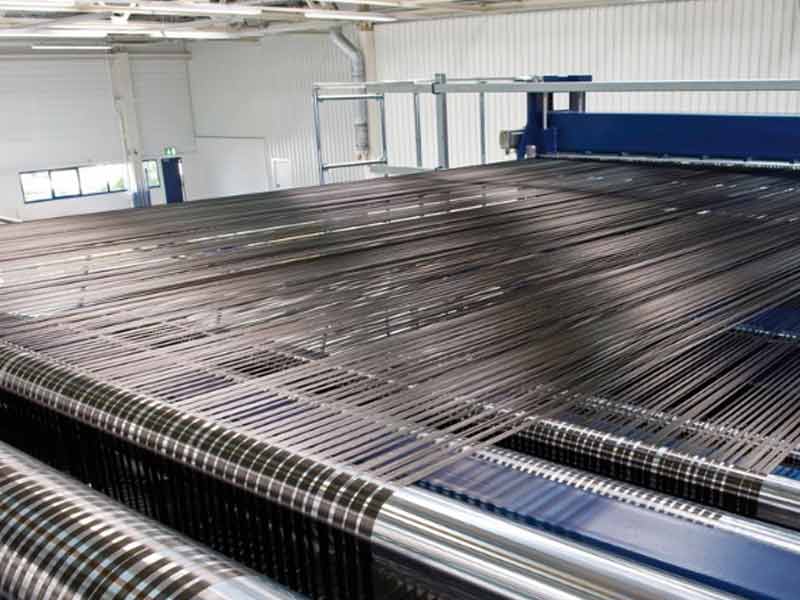
Carbon fiber manufacturing is the most energy-sensitive stage before composite processing begins.
PAN Precursor Production
PAN is the dominant precursor for structural carbon fiber. Its chemistry requires polymerization, spinning, stabilization, and careful control before carbonization.
Stabilization converts the precursor into a heat-resistant structure. If tension, atmosphere, or residence time drift, fiber alignment and final strength can suffer.
This stage affects environmental impact because off-spec precursor may be downgraded or scrapped. Consistent precursor quality improves conversion yield and reduces wasted furnace capacity.
High Temperature Carbonization
Carbonization removes non-carbon elements and develops the carbon-rich fiber structure. Furnaces require controlled inert atmospheres, stable line speed, and consistent thermal exposure.
If the profile is unstable, the tow can develop uneven properties or surface damage. These defects reduce composite reliability and may require downstream rejection.
Energy demand is significant because the process must maintain severe thermal conditions. Heat recovery, furnace insulation, and process uptime directly influence environmental performance.
Energy Mix and Process Emissions
The electricity and heat source strongly affect the environmental profile of carbon fiber. Renewable power or lower-carbon heat can reduce the footprint of identical fiber grades.
Process emissions also depend on precursor byproducts and exhaust treatment. Oxidation gases and carbonization effluent need capture, cleaning, and monitoring.
Manufacturers improve control through:
- Renewable or lower-carbon electricity
- Heat recovery from furnace systems
- Stable furnace loading and line speed
- Better insulation and process uptime
- Exhaust capture, cleaning, and monitoring
Poor utilization wastes energy because furnaces consume power even during inefficient operation.
Pitch Based and Bio Based Alternatives
Pitch based carbon fiber can provide very high stiffness for thermal or space applications. Its environmental profile depends on feedstock source, purification energy, and conversion yield.
Bio based precursors are being developed to reduce dependence on fossil feedstocks. They still need consistent molecular structure, fiber spinning quality, and stable carbonization behavior.
Alternative precursors are not automatically lower impact. They must meet mechanical requirements without increasing scrap, energy use, or process complexity.
| Precursor Type | Main Advantage | Environmental Concern |
|---|---|---|
| PAN based | Strong structural performance | High stabilization and carbonization energy |
| Pitch based | Very high stiffness and thermal performance | Feedstock and purification impact |
| Bio based | Lower fossil feedstock dependence | Process stability and yield control |
CFRP Processing Impact
Composite processing determines scrap level, cure efficiency, defect rate, and final part durability.
Prepreg, Dry Fabric, and Resin Infusion Waste
Prepreg provides controlled resin distribution and fiber alignment, but expired material becomes waste. Cold storage, cutting plans, and batch tracking reduce avoidable disposal.
Dry carbon fiber fabric avoids refrigerated resin storage and supports infusion routes. However, poor permeability control can cause dry spots, resin-rich zones, and rework.
Infusion waste includes resin lines, consumables, bleed media, and trimming scrap. Closed process planning reduces waste while maintaining laminate quality.
| Material Route | Waste Risk | Control Method |
|---|---|---|
| Prepreg | Expired material and ply offcuts | Cold storage and batch tracking |
| Dry fabric | Drape errors and dry spots | Permeability and preform control |
| Resin infusion | Resin lines and consumables | Closed process planning |
Autoclave, RTM, and Compression Molding Energy
Autoclave processing provides pressure and temperature uniformity for demanding CFRP parts. It also consumes significant energy through heating, pressurization, and long cycle control.
RTM injects resin into a closed mold and can reduce consumable waste. Flow simulation, vent placement, and preform compaction control voids and dry regions.
Compression molding can process sheet molding compounds or thermoplastic organosheets efficiently. Tool temperature, charge placement, and closing speed affect fiber movement and surface quality.
| Process | Main Strength | Main Impact Issue |
|---|---|---|
| Autoclave | High laminate quality | High energy and long cycles |
| RTM | Closed mold and lower consumables | Flow control and dry regions |
| Compression molding | Faster production potential | Fiber movement and tool heating |
Thermoset and Thermoplastic Resin Systems
Thermoset resins provide stable cured networks and established aerospace processing routes. Their crosslinked structure improves heat resistance but limits remelting at end of life.
Thermoplastic resin systems can be welded, reshaped, and more readily recycled. They need higher melt processing control and careful impregnation to avoid voids.
Resin selection affects environmental impact through cure energy, toughness, repair method, and recycling route. The matrix must match service temperature, damage tolerance, and production volume.
| Resin System | Processing Feature | End-of-Life Feature |
|---|---|---|
| Thermoset CFRP | Stable cure and high heat resistance | Difficult to remelt or reshape |
| Thermoplastic CFRP | Requires higher melt control | Easier welding and recycling |
Voids, Cure Defects, and Rejected Parts
Voids reduce interlaminar strength and can accelerate fatigue damage in a carbon fiber laminate. They form from trapped air, volatile release, poor compaction, or resin flow imbalance.
Cure defects include undercure, overcure, thermal gradients, and resin-rich areas. These issues cause dimensional drift, weak bonding, or reduced heat resistance.
Process controls include:
- Vacuum integrity checks
- Resin viscosity monitoring
- Tool temperature mapping
- Controlled compaction pressure
- Cure cycle documentation
Lower rejection rates reduce material waste and embodied emissions.
Carbon Fiber Recycling
Recycling can recover fiber value, but recovered products usually differ from continuous virgin reinforcement.
Mechanical Recycling
Mechanical recycling cuts or mills CFRP scrap into shorter reinforcement. It uses relatively simple equipment and avoids high chemical complexity.
The process damages fiber length and reduces alignment control. Recovered material is mainly used in compounds, mats, or nonwoven reinforcement.
Dust control and sizing compatibility are important process controls. Poor handling can reduce bonding and create workplace contamination risks.
Pyrolysis and Oxidation
Pyrolysis decomposes the polymer matrix in low-oxygen conditions and leaves carbon fiber behind. Oxidation removes resin through controlled exposure to reactive gas.
Both methods must balance resin removal with fiber property retention. Excessive exposure can damage the fiber surface and reduce composite performance.
Recovered fiber usually needs surface treatment or sizing before reuse. Consistent cleaning improves bonding with new thermoset or thermoplastic matrices.
Solvolysis and Chemical Recycling
Solvolysis uses solvents and catalysts to break down the resin matrix. It can recover cleaner fibers and sometimes useful resin-derived chemicals.
Process control focuses on solvent selection, pressure safety, reaction completeness, and washing quality. Incomplete matrix removal causes weak adhesion in the next composite.
Chemical recycling can be attractive for high-value CFRP waste. Its environmental value depends on solvent recovery, energy demand, and recovered fiber performance.
| Recycling Method | Recovered Format | Main Limitation |
|---|---|---|
| Mechanical recycling | Chopped or milled fiber | Shorter fiber length |
| Pyrolysis | Recovered carbon fiber | Surface damage risk |
| Oxidation | Cleaned fiber | Fiber strength loss risk |
| Solvolysis | Cleaner fiber and resin chemicals | Solvent recovery and cost |
Recycled Carbon Fiber Products
Recycled carbon fiber is commonly converted into:
- Chopped fiber
- Nonwoven mats
- Carbon fiber veil
- Reinforced pellets
- Compression molding compounds
These formats suit automotive panels, electronics housings, tooling boards, and sporting goods.
Designers must account for shorter fiber length and less controlled orientation. Parts should be tested for stiffness, impact resistance, and bonding performance.
Using recycled fiber is most effective when the product does not require continuous load paths. It still provides value where weight reduction and electrical properties matter.
Landfill Issues with Thermoset CFRP
Thermoset CFRP does not biodegrade or remelt under normal landfill conditions. The fiber and cured resin remain persistent.
Landfilling also loses the energy invested in precursor and carbonization. Recycling plans should be included in procurement specifications.
Lower Impact Carbon Fiber Design
Lower impact design starts with using less material while meeting structural and durability requirements.
Choose the Right Fiber Grade
Use the selected carbon fiber grade to match stiffness, strength, fatigue behavior, and cost. Over-specifying modulus or strength increases embodied energy without improving the part.
High modulus fiber helps stiffness-driven structures but can reduce damage tolerance. Standard modulus grades often suit general CFRP components with balanced properties.
Material qualification should include:
- Tensile strength testing
- Compression testing
- Interlaminar strength testing
- Fatigue and impact testing
- Environmental exposure testing
Correct grade selection reduces scrap, overdesign, and replacement frequency.
Optimize Tow Size and Laminate Design
Tow size affects drape, surface appearance, permeability, and fiber spreading. Fine tow improves detail and weave definition but can increase handling effort.
Larger tow can reduce fabric cost and improve deposition speed. It may create thicker bundles, print-through, or resin-rich channels in tight radii.
Laminate design should place fibers along principal load directions. Balanced stacking reduces warping, coupling, and unnecessary material use.
| Design Factor | Effect | Lower Impact Approach |
|---|---|---|
| Fine tow | Better detail and surface definition | Use only where needed |
| Larger tow | Faster deposition and lower fabric cost | Avoid tight radii issues |
| Fiber orientation | Controls load path efficiency | Align fibers with main loads |
| Stacking sequence | Affects warping and coupling | Use balanced laminate design |
Reduce Scrap and Machining Waste
Scrap reduction begins with nesting software, ply kitting, and controlled storage. Better nesting reduces offcuts before resin or labor is added.
Machining waste is controlled through:
- Sharp cutting tools
- Stable fixturing
- Dust extraction
- Correct feed strategy
- Controlled drilling and edge finishing
Poor carbon fiber cutting causes delamination, splintering, and rejected edges.
Near-net molding reduces trimming requirements and composite dust generation. It also improves environmental performance by converting more input material into finished parts.
Extend Service Life With Repair
Repair extends the useful life of a carbon fiber part and delays replacement. Inspection identifies delamination, impact damage, moisture ingress, and adhesive failure.
Common repair methods include:
- Bonded patches
- Scarf repairs
- Local laminate replacement
- Adhesive joint restoration
- Nondestructive inspection after repair
Repair quality depends on surface preparation, cure control, and nondestructive inspection.
A repairable design needs access, documented laminate schedules, and compatible resin systems. These choices reduce lifetime material consumption and disposal.
Carbon Fiber vs Other Materials
Material comparison should consider production impact, service savings, durability, repair, and recycling infrastructure.
Carbon Fiber vs Steel
Steel is energy intensive, but recycling systems are mature and widely available. It is often greener for stationary structures where weight has little effect.
Carbon fiber can outperform steel environmentally when moving mass dominates energy use. The CFRP design must avoid overbuilding and provide enough service life.
Steel also provides ductility and easy repair through conventional methods. Carbon fiber needs different inspection and bonding practices after impact.
Carbon Fiber vs Aluminum
Aluminum has established recycling loops and good corrosion resistance. Its production impact depends strongly on electricity source and recycled content.
Carbon fiber can provide lower weight and high fatigue resistance in specific structures. However, galvanic corrosion must be controlled when CFRP contacts aluminum.
Designers use isolation layers, sealants, or compatible fasteners to prevent corrosion. The greener choice depends on load case, service life, and recycling route.
Carbon Fiber vs Fiberglass
Fiberglass has lower manufacturing energy and lower material cost than carbon fiber. It can be environmentally favorable in non-weight-critical applications.
Carbon fiber provides higher stiffness and lower mass for the same load target. That advantage matters when reduced weight saves operational energy.
Both materials face challenges with thermoset recycling. Resin choice, part thickness, and recovery route strongly influence the final comparison.
| Material | Environmental Strength | Environmental Limitation |
|---|---|---|
| Steel | Mature recycling system | Heavy in moving structures |
| Aluminum | Good recycling loop | Production impact depends on electricity |
| Fiberglass | Lower manufacturing energy | Lower stiffness and thermoset recycling issues |
| Carbon fiber | High stiffness to weight ratio | Energy intensive production |
When Other Materials Are Greener?
Other materials are greener when they meet requirements with lower embodied impact and easier recycling. This often applies to static brackets, covers, and low-load panels.
Material selection should avoid using carbon fiber for appearance alone. A life cycle review should confirm a measurable service benefit.
Applications With Environmental Payback
Environmental payback is strongest when carbon fiber reduces energy consumption during long service.
Wind Turbine Blades
Carbon fiber can reduce blade mass while improving stiffness in long-span wind applications. Lower mass eases root loads, transport stresses, and pitch system demand.
Designers often place carbon fiber in spar caps or high-load regions. Glass fiber may remain in lower-load skins to balance impact and cost.
End-of-life planning is important because large blades are difficult to landfill. Recyclable resin systems and modular repair strategies improve the overall environmental case.
Aircraft Lightweighting
Aircraft structures benefit from carbon fiber because mass reduction lowers fuel or energy demand. The payback improves with long service and high utilization.
Aerospace CFRP requires strict control of prepreg storage, ply orientation, compaction, and cure traceability. Defects can compromise strength and cause costly rejection.
Nondestructive testing verifies laminate quality before service. Repair manuals and inspection intervals support long life and reduce replacement impact.
Electric Vehicle Lightweighting
Electric vehicles can benefit when lighter structures improve driving efficiency or increase payload capacity. The benefit depends on duty cycle and battery strategy.
Carbon fiber is most suitable for high-load beams, enclosures, and selected body structures. Recycled carbon fiber compounds can suit secondary parts with lower structural demand.
Thermoplastic CFRP can support faster forming and future recycling routes. Joining design must address adhesive durability, crash performance, and repair access.
| Application | Carbon Fiber Benefit | Environmental Payback Condition |
|---|---|---|
| Wind turbine blades | Lighter long-span structures | Long service and blade repair planning |
| Aircraft structures | Lower fuel or energy demand | High utilization and long service life |
| Electric vehicles | Lower mass and higher payload potential | Suitable duty cycle and repairable design |
FAQ
Is Carbon Fiber More Environmentally Friendly Than Fiberglass?
Not always. Carbon fiber can be greener when weight savings reduce energy use during long service.
Is Carbon Fiber Biodegradable?
No, carbon fiber is not biodegradable in normal conditions. Thermoset CFRP also resists natural breakdown.
Why is PAN Based Carbon Fiber Energy Intensive?
PAN based carbon fiber needs stabilization and carbonization under controlled atmospheres. These steps require sustained heat and process control.
Can Carbon Fiber Composites Be Recycled?
Yes, carbon fiber composites can be recycled through mechanical, thermal, or chemical methods. Recovered fiber usually returns in shorter formats.
Does Recycled Carbon Fiber Reduce Carbon Footprint?
It can reduce footprint by avoiding new precursor and carbonization demand. The benefit depends on recovery quality and reuse application.
When Does Lightweighting Offset Carbon Fiber Emissions?
Lightweighting offsets emissions when service energy savings exceed production impact. The part must last long enough to deliver that benefit.


